downloadGroupGroupnoun_press release_995423_000000 copyGroupnoun_Feed_96767_000000Group 19noun_pictures_1817522_000000Member company iconResource item iconStore item iconGroup 19Group 19noun_Photo_2085192_000000 Copynoun_presentation_2096081_000000Group 19Group Copy 7noun_webinar_692730_000000Path
Skip to main content
Strong global semiconductor industry growth is helping power rapid expansion of China’s IC manufacturers in 2018, and continuing technology innovation is inspiring the region’s optimism over the long term, said Du Shanshan, senior analyst of SEMI China, at the recent SEMI China Member Day. The chief driving force behind this year’s growth of China’s IC industry is its equipment and materials market, with the sector riding a wave of a strengthening industrial infrastructure, a rapid increase of wafer manufacturing capacity, global leadership in new fab projects and large memory investments, Shanshan added. NAURA, a leading domestic provider of high-end IC equipment, is seeing robust growth after its push to recruit highly skilled talent and bolster its technology infrastructure, customer service system and supply chain, said Zhou Yang, vice president of Procurement at NAURA, which hosted the event. Yang said the key to NAURA’s success has been its unblinking focus on technology, product quality, fast product delivery, responsiveness to customer needs, cost controls, and environmental and social responsibility. Before visiting a NAURA factory, attendees reflected on how China’s IC manufacturers, using equipment and materials sourced domestically, seized the opportunity of global semiconductor growth to drive rapid local expansion. Excited about the growth potential of China's chip industry, members expressed their commitment to contributing to its independence and self-reliance. SEMI China Membership Grows Opening SEMI China Member Day, SEMI China president Lung Chu highlighted another expansion – SEMI China’s membership growth to nearly 400 companies, behind only the U.S. and Japan. Chu credited the increase, in part, to the steady growth of the global semiconductor industry. Chu said the increase also stems from the recognition that SEMI China is the China semiconductor industry’s best partner for fulfilling its ambition of becoming a more prominent player on the world stage. SEMI China’s member services platform that includes exhibitions and conferences, industry technical standards, industry research and analysis, a publicity apparatus and a talent development initiative provides powerful ways for the industry to Connect, Collaborate and Innovate. The platform enabled SEMICON China 2018 to set a booth and visitor record for the event, with attendees numbering 91,252, a highly successful 32 percent year-over-year growth. More than 50 SEMI member companies attended the 2018 SEMI China Member Day on June 6th in Beijing to explore opportunities for the global and Chinese semiconductor industry. Cherry Sun is a marketing manager at SEMI China.
Read More
The Advanced Lithography TechXPOT at this year’s SEMICON West will explore progress in extreme ultraviolet lithography (EUVL), its economic viability for high-volume manufacturing (HVM) and other lithography solutions that will address the march to 5nm and onward to 3nm.As a prelude to the event, SEMI asked Neeraj Khanna, Global Head of the Patterning Customer Engagement Team at KLA-Tencor, a speaker at the TechXPOT, for insights about the readiness of inspection and metrology tools for EUVL applications at 5nm and 3nm. For a full list of speakers and program agenda, visit http://www.semiconwest.org/programs-catalog/lithography-5nm-and-below.Neeraj Khanna, Global Head of the Patterning Customer Engagement Team at KLA-TencorSEMI: In general, how would you characterize the readiness of inspection and metrology tools intended for EUVL applications at 5nm and 3nm? In particular, what are some of the remaining research and development challenges that need to be addressed for each of these nodes?Neeraj Khanna: KLA-Tencor is working closely with its customers to qualify and ramp EUV. Our suite of inspection, metrology and data analytic solutions are being implemented to enable EUV infrastructure readiness including, for example, new reticle and resist qualification, scanner qualification, and EUV ramp preparation. These EUV integration activities require process control systems that support a wide range of applications, including hotspot discovery, lithography modeling, focus/dose process window qualification, reticle print check, mask blank inspection, and process and tool monitoring.As with any major technology inflection, it is critical to understand sources of process variation to enable ramp at optimal yield. For example, stochastics result in random pattern variations, which have a major impact on EUV yield. To manage stochastics, IC manufacturers are deploying process control solutions that support fast modeling of stochastic variations coupled with high-sensitivity, high-coverage wafer defect inspection. Another example is a methodology called hybrid scanner utilization whereby, when EUV scanners are implemented in production, they will only be used for a few layers, while all other layers will be patterned with 193i scanners. This technique requires tighter control and monitoring of overlay budgets.SEMI: How are you able to achieve this tighter control and monitoring?NK: To understand why hybrid scanner utilization requires tighter control and monitoring of overlay budgets, it’s important to outline how this differs from current scanner implementation. For critical layers in current process flows using 193i lithography, pattern layers for a given wafer are printed using the same stage/chuck on the same scanner. The overlay performance achieved using this lithography strategy is called dedicated chuck overlay (DCO). Use of a dedicated scanner and chuck for lithography reduces inter-scanner and inter-chuck distortion effects, resulting in DCO overlay error of less than 1nm. When EUVL is first implemented in production, it will be used for a few layers – likely, cut masks and contacts with eventual migration to metal 1 layers. All other layers will be patterned with 193i scanners. This hybrid scanner operation eliminates any possibility of using a dedicated scanner and dedicated chuck to support tight overlay performance specifications. Instead, fabs will be forced to optimize mix-and-match overlay (MMO), with the overlay performance obtained using different scanners for printing different layers on a given wafer.With overlay specifications for advanced DRAM and logic at ~2.5nm, fabs will need to implement strict 193i-to-EUV scanner matching strategies or risk consuming 60 to100 percent of the overlay budget on just MMO. To achieve tighter overlay control and monitoring required for MMO, fabs need to implement dense, in-field overlay error measurements that feed into scanner fleet management systems. KLA-Tencor’s ATL™ overlay metrology system supports a high measurement speed and the use of small in-die targets, enabling dense in-field overlay measurements with high accuracy. Our 5D Analyzer® data analytic and management system includes scanner fleet management capability that enables automatic product-based corrections to minimize MMO error, helping fabs reduce the risk to yield loss associated with a 193i-EUV mixed scanner implementation. SEMI: What other challenges do you see coming to the fore at 5nm and 3nm?NK: Overall, the 5nm and beyond design nodes will face challenges associated with new lithography technology, potential new device structures and smaller pattern pitches. IC manufacturers will require process control solutions that not only identify process windows, but also monitor patterning parameters and defectivity at multiple points to identify process shifts. To monitor dynamic processes at these advanced nodes, inspection and metrology tools will need to have both sensitivity to critical parameters/defects and robustness to process variation in order to provide IC engineers with smart feedback for efficient control of their processes.SEMI: Could you elaborate on what will be required to monitor patterning parameters and defectivity at multiple points? How different will the techniques be at 5nm/3nm vs. at say, 7nm or 10nm?NK: As an example of monitoring at multiple points, consider the transition to EUV lithography. With EUV, the cost per scan goes up dramatically. Thus, IC manufacturers will monitor parameters at multiple points to maximize yield and minimize risk: EUV reticle qualification requires inspection and metrology throughout the entire flow from mask blank manufacturing, to the mask shop, to the IC fab. For the advanced design nodes associated with EUV, wafer qualification requires monitoring and control of wafer defectivity, shape and geometry throughout the wafer manufacturing process. It also requires control of fab incoming wafer qualification while ensuring that fab-wide processes are meeting defect and shape standards necessary for printing smaller feature sizes. EUV resist characterization and qualification requires comprehensive lithography simulation, wafer defect inspection, and film thickness and uniformity measurements to help reduce development time and prepare the litho stacks for production ramp. As EUV scanners are ramping, fabs are faced with finding any unknown particle sources within the new scanner chambers. This situation is driving the need for tighter and more frequent PWP (particles per wafer pass) chamber monitors to ensure scanner cleanliness. In addition, EUV scanner qualification requires reticle front and backside particle checks, and hotspot discovery and process window qualification using optical wafer defect inspection and e-beam review. EUV process monitoring encompasses overlay error monitoring, focus/dose monitoring, critical dimension (CD) and 3D device shape monitoring, and continuous process window monitoring. EUV inline defect monitoring and tool monitoring is important for reducing baseline defectivity in the litho cell for faster ramp, and for early identification of litho excursions in production. A critical part of this monitoring strategy is inline after develop inspection (ADI) monitoring, which is defect inspection on patterned wafers after printing and development of the resist ADI. Inline ADI innovations that find yield-critical defects allow fabs to reduce process issues, prevent at-risk wafers early in the process, and enable rework when excursions are found in production. As with past technology transitions, the implementation of multiple monitoring steps as part of a comprehensive process control strategy will be critical for a fab’s successful ramp of EUV.Debra Vogler, SEMI
Read More
New metrology and inspection technologies and new analysis approaches made possible by improving compute technology offer solutions to finding the increasingly subtle variations in materials and subsystems that meet specifications but still cause defects on the wafer. More collaboration across the supply chain is helping too. SEMICON West programs on materials and subsystems will address these issues. New metrology approaches needed to deal with process margin challenges As device process margins shrink and subtler materials variations cause unwanted deviations, the need for better monitoring of both surface and sub-surface material variations is driving a trend towards “metro-spection” – the convergence of metrology and inspection. “Device process margins have eroded to the point that traditional metrology strategies and techniques are no longer viable for controlling yield and parametric performance,” says Nanometrics Vice President Robert Fiordalice, who will speak in the materials program at SEMICON West. “Limited sampling capability, low throughput, insufficient sensitivity or the destructive nature of the techniques can often become problems. What’s more, deviations in material characteristics are not always determined by the initial quality of the material, but often arise from variations during the integration of the materials.” One new type of inline tool or line monitoring technology is Fourier Transform Infrared (FTIR) spectroscopy, traditionally used in quality control or tool characterization. Better sensitivity and higher throughput now enable rapid analysis and feedback for on-the-fly detection of subtle deviations in film properties that may compromise device performance or yield. More advanced analytics will help extract new information from old metrologyMore expensive metrology may not be required to identify subtle variations in in-spec materials that cause wafer defects. Today’s advanced compute capabilities now enable more sophisticated analysis of existing data and the identification of small but significant variations in raw materials and finished goods. The figure of merit (FoM) values presented in certificate of analysis (CoA) reports miss subtle variations in raw material properties. Of particular note is the reduction of molecular weight distributions to a mean, and standard deviation, whereas variations in the tails are associated with pattern defects. Advanced compute capabilities now allow the industry to step beyond the FoM in favor of more holistic measures, enabling predictive analysis of resist chemical variations associated with specific pattern defects. Source: JSR Micro“We often don’t need to find a new measure, but just a new way of looking at what we measure now,” says Jim Mulready, vice president of global quality assurance at JSR Micro. Mulready will speak in the SEMICON West program on materials defectivity issues. “The certificate of analysis reduces multiple measurements to a single figure of merit. But if we ignore all that raw data, we miss a chance to learn. One of our sayings in quality is ‘Customers don’t feel the average, they feel the variation.’ In many electronic materials, the quality of the raw material can have a big impact on the final performance, but the types of analysis needed to look at the tails of the distribution of these measures (such as molecular weight) in detail used to be really hard to do. Now it’s becoming increasingly straightforward and affordable.” Mulready says tools now available in the data processing sector enable the identification of subtle variations in materials that can cause defects on the wafer. These tools use methods like detailed subtractions of chromatography curves of polymer raw materials or analysis of tails of distributions of molecular weights. “Our job now is to drive these kinds of more sophisticated data analysis back into our chemical supply chain as well,” says Mulready. “We must work more closely with our suppliers to integrate their raw materials into our products. The reason the JSRs of the world exist is as a safety valve to reduce the variation from the chemical industry before it gets to the fab.”Continued collaboration with equipment suppliers required While the industry has been talking about the need for tighter collaboration between materials suppliers and equipment manufacturers for years, it still doesn’t always happen. “The material supplier and the equipment maker are tied together like kids in a three-legged race when we deliver an integrated system for consistent on-wafer performance,” says Cristina Chu, TEL/NEXX director of strategic business development, another speaker in the materials program. “When we introduce changes to the tool hardware, we need to make sure it doesn’t upset the system. Similarly, we need the material supplier to send a bottle over when a new chemistry formulation is under development. If a new chemistry runs into problems in the field, it will take much more time for both of us to fix it at the customer site. The toolmaker can provide a slightly different perspective on applications, while being more objective than a customer on how the formulation performs compared to earlier versions.”Regular and ongoing collaboration between chemistry suppliers and toolmakers enables the highest quality system solution to reach the customer. Chu notes that her team tries to maintain consistent collaborations with material suppliers across changes in organizations as the business environment changes. “For consistent on-wafer capabilities, we need a consistent collaboration process with chemistry suppliers. We need to meet with materials providers at a regular cadence throughout their development process. We need to check back with them as we scale up results from the coupon to the wafer level and to work out the kinks in the integrated solution together. The quality and consistency of our combined performance at the customer depends on ensuring the quality and consistency of our development and evaluation process as well.”Fabs and subsystems suppliers look to pilot data sharing program to improve process margins With ever tighter process margins, subtle variations in parameters that don’t appear in the specifications are also compromising results on the wafer, and neither the fab nor the supplier alone has the full information needed to improve performance. To help, a SEMI standards group is developing a protocol for a pilot program to standardize and automate some data sharing.The fab knows that performance is best with a particular parameter value, and knows when performance fluctuates, but often faces a black box problem with no way of knowing what exactly is wrong. In the rush to get the tool back up, the fab engineers may not get around to emailing the supplier about the issue for some time. The subsystems supplier, on the other hand, may know the cause of the variation, but likely has no way of knowing the critical parameters or ideal target values for the fab’s process. “In order for engineers to have constructive conversations about how to improve performance, we all need to exchange more information,” says Eric Bruce, Samsung Austin diffusion engineer, and co-chair of the SEMI Standards initiative addressing the issue, who will speak in the subsystems program at SEMICON West. A potential solution could be to create a standard and automated process to share particular data, agreed to in the purchasing contract, whereby the subsystems supplier shares more information about their parameters with the fab, and the fab in return gives feedback on what parameters work best to drive improved performance. The best place to start will likely be on parts that do not contain core yield-related IP, but where usage and lifetime information is useful.“We’re looking for people to participate in a pilot program to work together with suppliers to try sharing some information to improve performance,” says Bruce. “There’s a lot of this sharing in the backroom anyway, but this could make it fast and automated, and make everyone’s engineering job a lot easier.”Paula Doe, SEMI
Read More
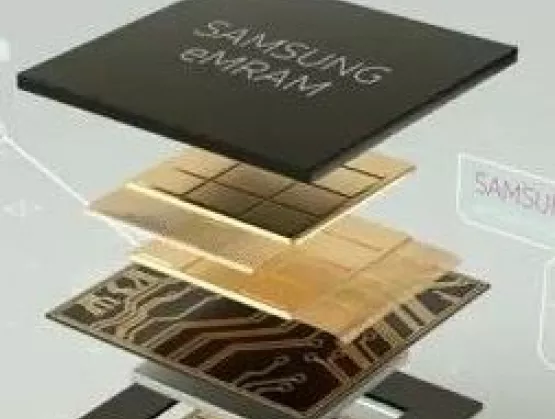
Per Arm, the industry's first eMRAM compiler IP is now on Samsung's 28nm FD-SOI technology. The announcement was made in a post by Kelvin Low, VP Marketing for ARM's Physical Design Group (read it here). He said that ARM has successfully completed their first eMRAM IP test chip tapeout. The Arm eMRAM compiler IP will be available from 4Q 2018 for lead partners. Samsung Foundry’s 28nm FD-SOI process technology is called 28FDS. eMRAM (which stands for embedded MagnetoResistive RAM) is a novel non-volatile memory (NVM) option positioned to replace incumbent NVM eFLASH, which has hit its limits in terms of speed, power, and scalability. Arm's new eMRAM compiler IP gives Samsung's 28FDS customers the flexibility to scale their memory needs based on the complexity of various use-cases, explains Low. “What drives the cost-effectiveness of this compiler IP is that eMRAM can be integrated with as few as three additional masks, while eFlash requires greater than 12 additional masks at 40nm and below,” he says. “Also, the eMRAM compiler can generate instances to replace Flash, Electrically Erasable Programmable Read-Only Memory (EEPROM) and slow SRAM/data buffer memories with a single non-volatile fast memory – particularly suited for cost- and power- sensitive IoT applications.” [caption id="attachment_11972" align="alignleft" width="300"] A key slide shown by Arm at the 2017 SOI Consortium's Silicon Valley Symposium (Courtesy: Arm and the SOI Consortium)[/caption] At the SOI Consortium's 2017 Silicon Valley Symposium, Arm said that they were stepping up their support of FD-SOI (read about that here) – and clearly they are! At that event, Arm VP Ron Moore gave a great presentation, which is freely available on our website: Low Power IP: Essential Ingredients for IoT Opportunities. Samsung, btw, has been offering 28FDS for about three years now. (ASN did a 3-part interview with Kelvin Low back in 2015 when he was a senior director of marketing for Samsung Foundry. It's still a useful read – you can get it here.) As of last fall, Samsung said it had taped out more than 40 products for various customers. And at the SOI Consortium's 2018 Silicon Valley Symposium, Hong Hoa, SVP said they'd already taped out another 20 this year (read about that here). https://youtu.be/EB14K8Gq5-w Samsung says the write speed of their eMRAM is 1000x faster than eFlash. They actually announced the industry's first eMRAM testchip tape-out milestone on 28FDS in September 2017 (you can read the press release here). They also did an eMRAM test chip with NXP. (BTW, Samsung has a really nice video explaining their eMRAM offering – you can see it above or on YouTube here.) As noted in ASN's Silicon Valley 2018 symposium coverage, the basic PDK for the Samsung 18nm FD-SOI process (18FDS) will be available in September 2018, with full production slated for fall of 2019. It will deliver a 24% increase in performance, a 38% decrease in power, and a 35% decrease in area for logic. RF for the 18FDS platform will be ready by the end of this year, and eMRAM beginning in 2019.
Read More
Dolphin Integration, a partner in the ENIAC THINGS2DO European FD-SOI project, showcased its achievements with PowerStudio™ during the project final review. Power Studio is Dolphin's cutting-edge EDA tool for safe Power Regulation Networks implementation. THINGS2DO, which stands for THIN but Great Silicon to Design Objects, was a 4-year, €120 million EU project (85% industry-funded) with over 40 partners that just finished up at the end of 2017. The goal was to build a design development ecosystem for FD-SOI. The project funded and supported the development of major FD SOI-based IPs and ASICs as well as EDA tools. (Another recent THINGS2DO announcement was Dream Chips’ ADAS SoC fabbed in GlobalFoundries’ 22FDX technology -- read about that here.) “Being involved in the THINGS2DO project was an opportunity for Dolphin Integration to start introducing FD-SOI in its automatic design methodologies,” said Frederic Poullet, Dolphin Integration’s CTO (read the press release here). “Dolphin Integration plans to offer a full suite of tools allowing its customers to implement right-on-first-pass Power Regulation Networks.” The company notes that THINGS2DO also proved that low power consumption makes FD-SOI a perfect fit for IoT and automotive applications. For instance, dynamic control of threshold voltage can be used to compensate for temperature variations, and to drive speed improvements by 200% in ultra-low voltage applications. Dolphin Integration provides energy efficient IPs and ASIC services dedicated to the low-power application market and supports its internal teams with tailor-made software tools. To address the specific needs of its customers in low-power design, Dolphin developed PowerStudio™, a global solution for the optimization of Power Regulation Networks (PRNet) to be used at an early stage of the SoC design process. In particular, it addresses new design challenges in noise and power supply integrity. The first module of PowerStudio™ will also embed architecture optimization features at the schematic level, in terms of FoM-based cost optimization, mode management, margin cuts and integrability rate-based risk optimization. Btw, Dolphin Integration Director Frederic Renoux gave an excellent great presentation at an SOI Consortium event in Nanjing, China last year, entitled Embedding power regulation activity control networks for best SoC PPA. Dolphin Integration joined Global foundries’ FDXcelerator™ Program last year (read the press release here) to streamline design in 22FDX®. "Our comprehensive and robust library of voltage regulators, power gating cells and logic modules, enables to deal cost-effectively and securely with power distribution, power gating, power monitoring and power control of any SoC design in 22FDX," Michel Depeyrot, Dolphin Integration's Chairman, said at the time. "As connected devices sleep most of their time, users of 22FDX also benefit from our ultra-low power and accurate oscillators to design an always-on RTC which consumes as little as 60 nA." See the Dolphin Integration website for the full catalog of their IP, EDA and ASIC/SoC service offerings, including for GF's 22FDX.
Read More
For medtech applications to flourish, sensors need a supporting infrastructure that translates the data they harvest into actionable insights, says Qualcomm Life director of business development Gene Dantsker, who will speak about the future of digital healthcare in the Medtech program at SEMICON West. “Rarely can one device give a complete diagnosis,” he notes. “What’s missing is the integration of all the sensor data into prescriptive information.” The maturing medtech sector has developed to the point where sensors can now capture massive amounts of data, conveniently collected from people via mobile devices. The sector now has higher compute capacity to process the data, and improving software can produce actionable insight from the information. The next challenge is to seamlessly integrate these components into legacy medical systems without disrupting existing workflow. “Doctors and nurses don’t have time for disruptive technology – a new system has to be invisible and frictionless to use, with one or fewer buttons, no training and truly automatic Bluetooth-like pairing,” he says. “So device makers need to pack all system intelligence into the circuits and software.”Getting actionable healthcare information from sensors requires integration into the existing medical infrastructure. Source: Qualcomm LifeOne interesting example is United Healthcare’s use of the Qualcomm Life infrastructure to collect data from the fitness trackers of 350,000 patients. The insurance company then pays users $4 a day, or ~$1500 a year, for standing, walking six times a day and other behaviors that clinical evidence shows will both improve patient health and reduce healthcare costs. “It’s a perfect storm of motivations for all stakeholders,” he says.Next hot MEMS topics: Piezoelectric devices, environmental sensors, near-zero power standbyWith sensor technology continuing to evolve, look for coming innovations in MEMS in piezoelectric devices, environmental sensors and near zero-power standby devices, says Alissa Fitzgerald, Founder and Managing Member of A.M. Fitzgerald and Associates, who will provide an update on emerging sensor technologies in the MEMS program at SEMICON West.Piezoelectric devices can potentially be more stable and perhaps even easier to ramp to volume than capacitive ones, with AlN devices for microphones and ultrasonic sensors finding quick success. Now the maturing infrastructure for lead zirconate titantate (PZT) is enabling the scaling of production of higher performing piezo material with thin film deposition equipment from suppliers like Ulvac Technologies and Solmates and in foundry processes at Silex and STMicroelectronics, she notes.In academic research, where most new MEMS emerge, market interest is driving development of environmental sensors and zero-power standby devices. With demand for environmental monitoring growing, much work is focusing on technologies that improve the sensitivity, selectivity and time of response of gas and particulate sensors. Research and funding is also focusing on zero or near-zero power standby sensors, using open circuits that draw no power until a physical stimulus such as vibration or heat wakes them up.MEMS, however, likely won’t find as much of a market in autonomous vehicles as once thought. “While the automotive sensor market will need many optical sensors, MEMS players are competing with other optical and mechanical solutions,” says Fitzgerald. “And here the usual MEMS advantage of small size may not matter much, and the devices will have to meet the challenging automotive requirements for extreme ruggedness.”Paula Doe, SEMI
Read More
What’s next for smarter, more connected electronics manufacturing - Part 3 The fast-maturing infrastructure now enabling analysis of exponentially larger data volumes brings the microelectronics industry to an inflection point, where the winning companies will be the first to master the use of this data to solve the industry’s emerging challenges. SEMI expands its coverage of these vital issues with a Smart Manufacturing Pavilion and three days of talks SEMICON West, July 10-12 in San Francisco. While deep learning is starting to be applied to image recognition for wafer inspection, it is also being considered for sequential pattern recognition in order to evaluate equipment parameter traces. The next emerging applications will start to use those learned patterns to predict outcomes, and then use those predictions to automate process control. One early application of deep learning is IC process development. “People don’t think of research and development as the first place to automate, but it’s where applying our digitization and simulation has first had impact,” says David Fried, Coventor vice president of Computational Products. He noted that insertion is easier in the lab than in the fab. Technology at 10nm and beyond is now so complex that companies at the leading edge must use process modeling to understand the effect of process variation on their designs. Learning cycles can now be accelerated during development by simulating 10,000 digital wafers instead of running 25 actual wafers during screening, Fried says. Applying structured analysis and machine learning to the data simplifies optimization across the 500 or more interrelated process steps. Coventor has recently introduced a statistical analysis package that aids the design and analysis of process variation experiments by using large volumes of data from its models. Fried says these models are next being used to accelerate the yield ramp in manufacturing. Digital simulation also could speed development of high-mix, lower value products While digital twins are best known for their use in complex, high value products like jet engines, the simulation technology could also enable the electronic manufacturing services (EMS) sector to reduce the time, cost and risk of developing its high mix of products. “The EMS sector’s use of digital twins will be vital for it to smooth the move of CAD/CAM digital design data for so many different products into manufacturing, and to accelerate validation testing of designs and products by doing more of it in the virtual world,” says Dan Gamota, vice president of Engineering and Technical Services at Jabil. Gamota also highlights the push for traceability from the automotive and healthcare markets, where the digital models could be used to quickly assure that the design was built exactly as specified. “In the past year, traceability has evolved from just ‘nice to have’ to ‘how to achieve,’” he adds. “Companies are expecting it, but aren’t willing to accept the cost and risk of doing it alone. We need the community to discuss realistic implementations, identify the most critical elements and bring together the ecosystem partners to build baseline reference architectures for key digital building blocks. The community also needs to assure the reliable flow of data among the electronic manufacturing segments from semiconductor to OSAT to EMS.” Predictive maintenance and virtual metrology applications could mature in next few years While predictive maintenance initially seemed a likely early application of machine learning in factories, it remains a challenge for the electronics sector. “The difficulty is that it’s not clear where to get the most bang for the buck,” says Tom Ho, president of BISTel America, noting that it may make the most sense to track the failure performance of a single expensive part, like an electrostatic chuck, since predicting the failure performance of a whole complex system like an etcher is much harder. “Collecting enough data from all failure types, including especially the rare events, is difficult unless you have a long history of a lot of tools,” adds Doug Suerich, PEER Group product evangelist. “The gain from collecting performance information from many tools across the industry could be big, but many companies still need to overcome concerns around exposing their IP.” Another big opportunity for prediction is virtual metrology – predicting the wafer outcome from the process or sensor data with enough accuracy to replace the physical metrology. “Virtual metrology is improving, and since metrology can be slow and expensive, any reduction could mean a huge potential savings,” says Suerich. “But it is still seen as too scary for many companies. Two to three years from now, companies will expand the practice from lower risk areas into processes that require more confidence in the results.” Moving beyond prediction to automated control needs digital models Once the results are predicted, the model can be used to control or automatically optimize a process and enable the system to learn by itself, usually by reinforcement learning on a digital model. The model can then independently make adjustments to optimize the manufacturing process. “Automated process development is getting close now. Instead of smart guys turning the knobs, deep learning is automating the smart tuning,” says Suerich, suggesting the industry could see widespread adoption in as little as two to three years. This type of machine learning needs a good digital model, and masses of data for learning. One approach uses human experts to build a physics-based model of the clearly understood parts of the process, then turns to deep machine learning to optimize the lesser-understood variables. The alternative, the data-first approach, runs a computer algorithm to suggest the solution purely from data, without human input, and then relies on the human to evaluate the usefulness of the results. Modeling digital twins of wafers could enable automated process control, chamber matching, and fleet matching, says Fried. If every wafer had its own virtual twin with all the upstream metrology and structural information needed to make equipment control decisions, it could feed forward that information to enable the seamless transition from one step in the process to another based on understanding their complex interrelationships. This could potentially improve uniformity across wafers and equipment, and reduce the need for metrology, he argues. Moving metrology sensors into the chamber will also require model-based algorithms to enable dynamic process control in close to real time, says Fried. These algorithms will be needed to acquire, parse, and process the data at high speed, and then to choose how to adjust the controls. “There will be a model behind collecting and interpreting the metrology data,” he notes. “That’s a really rich vein for improvements in process control.” “The end goal is to collect equipment data in real time, analyze it with AI, and send back controls to optimize manufacturing processes,” Jabil’s Gamota says. “This requires a robust architecture for communication between equipment and consistent formats for data collection and analysis. But the cost and complexity of this heavy lifting is too great for any one company to do alone. We need a consensus-based architecture for ingesting, analyzing and acting on the data.” SEMI tests data transfer protocols, benchmarks best practices SEMI is launching a smart data project to identify the various data transfer protocols needed for inter-company communications. The project will feature a proof-of-concept model in a development fab to produce verifiable results so SEMI can better understand how different approaches meet member needs. SEMI’s smart manufacturing technology communities and the Fab Owners Alliance are also benchmarking current smart manufacturing practices in the microelectronics industry to help SEMI members better understand the path forward and potential return on investment. Speakers over all three days at SEMICON West addressing these issues include Active Layer Parametrics, Applied Materials, Applied Research Photonics, ASML, Bosch Rexroth, Cimetrix, Coventor, ECI Technologies, Edwards Vacuum, Final Phase Systems, GE Digital, Infineon, Jabil, Lam Research, Osaro, Otosense, PEER Group, Qualcomm, Rockwell Automation, Rudolph Technologies, Schneider Electric, Seagate, Siemens, Stanford University, TEL, TIBCO Software. See semiconwest.org. What’s next for smarter, more connected electronics manufacturing - Part 1 What’s next for smarter, more connected electronics manufacturing - Part 2 Paula Doe, SEMI
Read More
With artificial intelligence (AI) rapidly evolving, look for applications like voice recognition and image recognition to get more efficient, more affordable, and far more common in a variety of products over the next few years. This growth in applications will drive demand for new architectures that deliver the higher performance and lower power consumption required for widespread AI adoption. “The challenge for AI at the edge is to optimize the whole system-on-a-chip architecture and its components, all the way to semiconductor technology IP blocks, to process complex AI workloads quickly and at low power,” says Qualcomm Technologies Senior Director of Engineering Evgeni Gousev, who will provide an update on the progress of AI at the edge in a Data and AI program at SEMICON West, July 10-12 in San Francisco. Qualcomm Snapdragon 845 uses heterogeneous computing across the CPU, GPU, and DSP for power-efficient processing for constantly evolving AI models. Source: QualcommA system approach that optimizes across hardware, software, and algorithms is necessary to deliver the ultra-low power – to a sub 1-milliwatt level, low enough to enable always-on machine vision processing – for the usually energy-intensive AI computing. From the chip architecture perspective, processing AI workloads with the most appropriate engine, such as the CPU, GPU, and DSP with dedicated hardware acceleration, provides the best power efficiency – and flexibility for dealing with rapidly changing AI models and growing diversity of applications.“So far it’s been largely a brute force approach using conventional architectures and cloud-based infrastructure,” says Evgeni. “But we’re going to run out of brute force options, so future opportunities lie in developing innovative architectures, dedicated hardware, new algorithms, and new software. Innovation will be especially important for AI at the edge and applications requiring always-on functionality. Training is mostly in the cloud now, but in the near future it will start migrating to the device as the algorithms and hardware improve. AI at the edge will also remove some privacy concerns, an increasingly important issue for data collection and management.”Practical AI applications at the edge where resources are constrained run the gamut, spanning smartphones, drones, autonomous vehicles, virtual reality, augmented reality and smart home solutions such as connected cameras. “More AI on the edge will create a huge opportunity for the whole ecosystem – chip designers, semiconductor and device manufacturers, applications developers, and data and service providers. And it’s going to make a significant impact on the way we work, live, and interact with the world around us,” Evgeni said.Future generations of chips may need more disruptive systems-level change to handle high data volumes with low power A next-generation solution for handling the massive proliferation of AI data could be a nanotechnology system, such as the collaborative N3XT (Nano-Engineered Computing Systems Technology) project, led by H.S. Philip Wong and Subhasish Mitra at Stanford. “Even with next-generation scaling of transistors and new memory chips, the bottlenecks in moving data in and out of memory for processing will remain,” says Mitra, another speaker in the SEMICON West program. “The true benefits of nanotechnology will only come from new architectures enabled by nanosystems. One thing we are certain of is that massively more capable and more energy-efficient systems will be necessary for almost any future application, so we will need to think about system-level improvements.” Major improvement in handling high volumes of data with low high energy use will require system-level improvements, such as monolithic 3D integration of carbon nanotube transistors in the multi-campus N3XT chip research effort. Source: Stanford UniversityThat means carbon nanotube transistors for logic, high density non-volatile MRAM and ReRAM for memory, fine-grained monolithic 3D for integration, new architectures for computation immersed in memory, and new materials for heat removal. “The N3XT approach is key for the 1000X energy efficiency needed,” says Mitra.Researchers have demonstrated improvements in all these areas, including multiple hardware nanosystem prototypes targeting AI applications. The researchers have transferred multiple layers of as-grown carbon nanotubes to the target wafer to significantly improve CNT density and have also developed a low-power TiN/HfOx/Pt ReRAM. The low-temperature CNT and ReRAM processes enable multiple vertical layers to be grown on top of one another for ultra-dense and fine-grained monolithic 3D integration. Other speakers at the Data and AI TechXpot include Fram Akiki, VP Electronics, Siemens; Hariharan Ananthanarayanan, motion planning engineer, Osaro; and David Haynes, Sr. director, strategic marketing, Lam Research. See SEMICONWest.org.Paula Doe, SEMI
Read More
What’s next for smarter, more connected electronics manufacturing - Part 2The fast-maturing infrastructure now enabling applications for big data and artificial intelligence means disruptive change not just at individual companies but also in data connections among companies across the microelectronics manufacturing value chain. SEMI checked in with some leading players on the changes they see coming in the next several years for this article series. The trade group is expanding its programming on smart manufacturing to address these industry-wide developments at SEMICON West, July 10-12 in San Francisco.“The ramp of EUV, and the smaller geometries and smaller process margins, will drive an exponential increase in the amount of metrology data to manage,” says Neal Callan, ASML vice president, Silicon Valley. Callan notes that moving to multibeam e-beam inspection will increase data volume from megabytes per second to gigabytes per second and from thousands of data points to millions of data points. “The process is so tight and the margin so small that stochastic variation, or noise, becomes more dominant – at least it’s noise until we can learn to understand and control it. And understanding and controlling this variation will be key to delivering 5nm patterning,” he says.Single-beam e-beam inspection is already driving large increases in data as engineers extend the slow technology to broad, high-speed defect metrology applications by more intelligently instructing the system where to look for problems. Callan says ASML is now using the scanner data on wafer focus, alignment and leveling. The company is also using the computational lithography model from the design to identify the smallest process windows in the pattern that are most likely to see problems. The model then quantifies the number and significance of those instances.“The collection of all this diverse data means that tools will need to be plug-and-play so all tool data is instantly available to all systems and software,” says Doug Suerich, PEER Group product evangelist. “We need tools that can be discovered automatically by the network so it can start slurping up data immediately. The adoption of the Interface A (EDA) standard is accelerating and fabs are starting to ask for it. The proliferation of sensors also needs to self-discover. If you are going to add thousands of new sensors into a facility, you can’t afford a time-consuming integration process.”“We are now seeing that engineers are greedy for more data – if they can get the data, it’s becoming a need-to-have,” adds Tom Ho, BISTel America president. “Getting more data from more sensors, from the sensors on the tool that are not being fully utilized, and from untapped data sources like vibration is another big coming opportunity.” Process complexity drives demand for feed-forward between silos with computational models ASML co-optimizes its scanner process with etch and reticle process steps. Source: ASML In addition to the drive for trace-back of data, the increasing complexity of interrelated processes is also driving demand for feed-forward of data. “Feed-forward is becoming more important,” notes Ho. He points to the example of 3D NAND features, now getting so deep that identifying the layer being measured is a challenge unless the signal at the step before can be recognized. “We need partnerships with our peers to understand how to take advantage of the sensors they use, integrate them with our data, and then feed-forward corrections to the other systems,” concurs Callan. “To drive the best CD uniformity and overlay, we need to co-optimize litho and etch,” agrees Henk Niesing, ASML director of product management. He notes that the company is working with etcher makers to measure the overlay and CD, decompose the finger prints, and then use models to steer automated control that best adjusts both the scanner and the etcher. ASML is also working with Zeiss on co-optimization between the scanner and the reticle to make even higher-order corrections by locally modifying the reticle.These higher-order corrections, applied on each exposed field, drive the need for even more data, and at higher speed but without higher cost, notes Jan Mulkens, ASML senior fellow. These corrections increase demand for computational metrology, which combines various metrology sources with physics and deep learning models trained on real data to predict and control process results in real time. “We’re working on computational metrology to ideally use all the knobs we have in the fab,” he says. So far this effort has largely involved linking data between two companies. More consistent data formats would enable data exchange to be extended to more companies. “The software versions also need to be managed for upgrades so they still match after one party updates the system on its tool,” notes Niesing. Speakers on these issues of smart manufacturing and data handling at SEMICON West include Active Layer Parametrics, Applied Materials, Applied Research Photonics, ASML, Cimetrix, Coventor, ECI Technologies, Edwards Vacuum, Final Phase Systems, GE Digital, Infineon, Jabil, Lam Research, Osaro, Otosense, PEER Group, Rockwell Automation, Rudolph Technologies, Schneider Electric, Seagate, Seimens, Stanford University, TEL, TIBCO Software. See semiconwest.org.What’s next for smarter, more connected electronics manufacturing - Part 1What’s next for smarter, more connected electronics manufacturing - Part 3Paul Doe, SEMI
Read More
Part 2 of this two-part piece examines the potential benefits to be realized by pairing human Subject Matter Experts with smart silicon assistants, and what these new arrangements mean for semiconductor device manufacturing. Part 1 explores best-practice perspectives on collecting and utilizing smart data in industries outside semiconductor manufacturing, one of the important takeaways from the Smart Manufacturing panel discussion at SEMI ASMC 2018. So what does this observation (i.e. the field of medicine, in what seems at first glance a big data environment, is really just clusters and clusters of loose small data connected by the collective neural network of highly trained doctors and their colleagues) mean for semiconductor manufacturing? We think it means we need to apply the same level of intense focus that we already devote to instrumented data collection and analytics in the fab to something more: we need to better capture the vast expertise of our engineering and operational talent in semiconductor manufacturing. We think we need to record what the subject matter experts (SMEs) in the fab see, hear, and think as they investigate yield excursions or machine-down problems. We need to effectively combine product, process, equipment and component subject matter expertise / subject matter experts (SME) with big data analytics to more effectively solve manufacturing problems, be they killer or be they chronic. And we must provide structured methods for incorporating inputs from and active participation of SMEs throughout the data analysis lifecycle, from collection and aggregation, through filtering, feature extraction, analysis and optimization. Some of the challenge will be in just how do we make it easy to gather information from SMEs in real time, while standing in front of equipment in the fab. Internet of Things (Iot) devices are emerging to capture and label images and sounds to enable machine learning algorithms to recognize and help diagnose manufacturing problems based on sight and sound, complementing the instrumented data. But we also need to record the thought processes our human SMEs go through in those investigations – perhaps by the SMEs talking to a smart AI-based conversational assistant who helps make “rounds.” Doing contextual analysis on this added data, combined with the instrumented data, will create the equation Human + Machine = AI (Awesome Insight). Sounds reasonable, right? We think artificial intelligence becomes too artificial if you leave the human out of the equation. AI should be augmented intelligence, where we take the expertise and creativity of the human, and combine it with the rapid computational capabilities of the computer, in order to put problem identification and solutions on steroids. But with the already huge advancements to date in data analytics, cloud, and the emergence of AI, why do improvements in quality, machine utilization, and the implementation of predictive analytics in semiconductor manufacturing seem to be creeping along incrementally, and not appearing as dramatic, step-function improvements? Call it Smart Manufacturing, call it Connected Enterprise, call it Advanced Manufacturing, or Analytics, or Cloud, or the Digital Twin … there are no shortages of terms, philosophies, and technologies available, but why aren’t we seeing their rapid adoption? It could be it’s the downside that comes with needing people. “Good business leaders create a vision, articulate the vision, passionately own the vision, and relentlessly drive it to completion.” Jack Welch. We see from other industries that smart manufacturing conversations originating with the executives of a company thinking to implement smart manufacturing programs lead to vision; however, we also see from other industries, and from our own, that realizing this vision has often been a challenge. Why is that? One reason may be that the people who are personally vested in solutions they implemented in the past, as well as those who follow a pattern of ‘how we’ve always done things’, create, inadvertently or not, persistent internal barriers hindering innovative action. Another may be that engagements with the working engineers and managers charged to be smart manufacturing implementers leads to the pursuit of low-hanging fruit, and cautious investments, that often utilize solutions that ultimately cannot scale and integrate. Not to mention the disadvantage of dealing with the legacy equipment, the legacy networks, the traditional thinking, and the lack of consistency in metrics adding to the confusion. Addressing all these barriers requires an alignment in strategy and execution, along with a plan to support the overall vision, often across the entire enterprise, which is no small matter. And then there are the standards. Having and adhering to standards in control solutions, networks, and data becomes critical in achieving real benefits from smart manufacturing. And data security. One of the other big impediments in the smart manufacturing transformation is data and IP security, another key concern (maybe the most significant) preventing us from moving forward more quickly (e.g. to cloud-based solutions) in our industry. More about that in a follow-up. Achieving synergy across all of manufacturing, from connecting equipment horizontally, through the production system (machines processes), and vertically, through enterprise systems and across production facilities, can only occur if we build standards, security, infrastructure, and human engagement throughout our ecosystem and supply chain. In simple form, the steps to do so include connecting assets, collecting and contextualizing data, and then driving business transformation with actionable insights gained from the data. With impact on every function, and every person, in the enterprise, from equipment operators in the fab through the C-Suite in HQ. Maintenance, Engineering, R D, Operations, Scheduling, IT, Procurement, Finance, HR all contribute, collaborate and benefit. Regardless of the technology, from device level analytics to predictive maintenance and optimization, the people that reside in these disparate groups need to come together with the smart machines to create a common strategy to achieve transformational results. Aligning an enterprise’s goals with its human capital is paramount to success. Therefore, we must challenge our team members and ourselves to work outside our comfort zones, and we need to be forever aware of the need for us to grow with the technology. Smart manufacturing is not necessarily about having fewer people in the fab, but it does suggest having people in the fab, perhaps with different, or upgraded, skill sets, who are even more efficient in their roles as a result of the boost they are getting from Industry 4.0. Fortunately, we now have techniques that let us combine the best, brightest, and latest and greatest analytics with our invaluable SMEs throughout the data analysis lifecycle. We’ll not only be able to deliver higher quality semiconductor manufacturing solutions all in all, but we’ll also be providing methods to more easily distribute, scale, maintain, and continually refine those hard-earned solutions. We expect that subject matter experts will continue to put the “smart” in machine-based smart manufacturing today, and for the foreseeable future. SME contributions are not an option, but, rather, an imperative for ensuring a semiconductor manufacturer’s sustained prosperity, much less its survival. Nancy Greco (IBM Watson), Dave Mayewski (Rockwell Automation), James Moyne (University of Michigan / Applied Materials), and Paul Werbaneth (Intevac, Inc.), along with Julie Jacob (Ernst Young), and Carson Henry (Micron Technology), were members of the SEMI ASMC 2018 panel discussing Industry 4.0 and the Future of Commercial Semiconductor Device Manufacturing. All opinions here are purely our own. Please contact Paul Werbaneth via email at [email protected]. The SEMICON West (July 9-11, 2018, in San Francisco) Smart Manufacturing Pavilion features working production equipment on the floor and three full days of speakers providing insights on building the infrastructure needed to enable AI. Equipment from Bosch Rexroth, Cimetrix, Rudolph Technologies, INFICON, Final Phase Systems, OMRON, DISCO and Edwards Vacuum will showcase cutting-edge smart manufacturing technologies. For information on the SEMI Smart Manufacturing initiative and how to get involved, please click here.
Read More